8011 vs 1235 Aluminium Foil: Which Alloy Should You Specify?
Both alloys are standard for thin foil, but they behave differently in food contact, laminating and forming. Here is how to choose between them.
Both alloys are standard for thin foil, but they behave differently in food contact, laminating and forming. Here is how to choose between them.
8011 and 1235 are the two alloys that appear most often on thin gauge foil enquiries. The choice affects strength, food contact approval, how the foil laminates, and how much you pay.
Why is 1235 called the pure foil alloy?
Converters reach for 1235 whenever a clean, predictable web matters more than load-bearing strength.
1235 is essentially unalloyed aluminium, around 99.35 percent pure. Its low impurity content makes it the preferred choice for food contact, laminating and lidding, where consistent barrier performance and cleanliness matter more than mechanical strength.
Dive deeper
Because 1235 carries almost no deliberate alloying additions, its internal structure stays simple and predictable, and that simplicity is exactly what a converter wants from a light gauge web. The foil deforms evenly, unwinds cleanly and is far less likely to tear when it runs across rollers at speed. It rolls down to very light gauges reliably, which is why the thinnest converter foil is usually 1235. If your application is wrapping, laminating or lidding, start here. Because there is so little alloying content, odour and taint risk tend to stay low, which matters when the foil sits directly against a food surface for months at a time.
There is a practical limit, though. A nearly pure foil is relatively soft and offers little stiffness of its own, so it can support a barrier but not a shape. The moment a package has to hold a profile, survive a press or carry a load, the conversation moves to a stronger grade. If you already know this is the one you want, the specification detail lives on the 1235 aluminium foil page, where gauge and temper options are listed. Everything else in this comparison is really about finding that boundary between cleanliness and structural support in your own product.
Why is 8011 called the workhorse?
Where 1235 is a specialist, 8011 is the generalist that keeps forming and packaging lines moving.
8011 adds iron and silicon, which raises strength and improves behaviour during forming and baking. It is the standard alloy for household foil, foil containers and semi-rigid food packaging, and it holds up better when the foil is embossed or pressed.
Dive deeper
Those two additions are modest, but they change how the metal behaves after it leaves the mill. Iron and silicon restrict grain growth and give the foil a stiffer, springier feel, so a thin web can be creased, folded and pressed without collapsing. That is why the same grade turns up in households, in catering kitchens and in semi-rigid packaging: the foil has enough backbone to be handled by a person or by a machine without losing the shape it was given. A household roll survives being pulled, torn and wrapped around an awkward object without splitting, and that is exactly the sort of everyday punishment a softer grade would struggle with.
The trade-off is a slightly less clean metallurgy than a near pure grade, which is why 8011 is normally chosen for formed or handled products rather than for the most sensitive barrier work. Temper also matters here: the same 8011 can be supplied in a range of hardnesses, and the one you pick decides whether the foil presses crisply or tears at the die. Buyers who need a formed container usually specify the grade alongside the temper, and the 8011 aluminium foil sheet lists the combinations we hold most often. That single choice often decides the whole forming trial.
How do 8011 and 1235 compare side by side?
Put the two grades next to each other and the differences can be described without a single number.
1235 is softer and cleaner, so it suits thin, flat webs that must stay low in odour. 8011 is stronger and stiffer, so it suits formed, pressed and embossed parts. One favours barrier and lidding; the other favours containers and retail rolls.
Dive deeper
The cleanest way to compare them is by asking what has to happen to the foil after it is unwound. A converter who laminates a light web to paper or film, or who needs a lidding stock that peels and seals predictably, will usually favour the nearly pure grade, because nothing in the metal interferes with the barrier or the seal. A converter who forms a tray, presses a lid or embosses a household roll needs the metal to resist the tool, and that is where the alloyed grade earns its place. The same logic applies when a single product needs two different layers: the structural layer and the barrier layer do not have to be made from the same grade.
It also helps to think about failure modes. A near pure web is more likely to stretch or crease unexpectedly under tension, while an alloyed web is more likely to resist deformation but can fight a delicate forming tool. Neither behaviour is wrong; each is a match for a different job, and a misjudged choice usually shows up as scrap rather than as a dramatic break. The general principles behind these trade-offs are set out in the background material on aluminium foil, which explains how gauge and alloying affect handling.
How do you decide between 8011 and 1235?
Most projects do not have to pick one grade for everything; the decision usually follows the part.
In practice, most buyers end up ordering both: 1235 for the converter roll and 8011 for the retail product. We supply both in our food and household foil range, and you can compare thickness options on the aluminium foil roll page.
Dive deeper
Start with the end use, then work backwards. If the foil becomes part of a laminate, a sachet or a lidding film, and it never has to hold its own shape, the near pure grade is normally the safer default. If the foil is formed into a tray, wrapped around a product under pressure, or handled by a shopper, the stronger grade is normally the safer default. Once that first question is answered, the remaining decisions are about thickness, temper, width and finish rather than about metallurgy, and they are usually quicker to settle.
The second useful question is about tolerance. A forming operation usually needs a tighter thickness window than a wrapping operation, because the die and the press are set for one gauge and a variation shows up as a wrinkle or a thin patch. Buyers who have not fixed the alloy yet often find that the choice becomes obvious once they write down the thickness range and the temper they actually need on the line. If both grades still look plausible, order a trial quantity of each and compare them on your own equipment before committing to a full schedule. Our engineers are happy to talk through that trial.
How do the two alloys behave in laminating?
Laminating rewards a clean, even web more than it rewards strength, and that tilts the choice.
1235 is the usual starting point for laminating because it unwinds flat and keeps odour and taint risk low. 8011 appears when the laminate needs extra stiffness or a formed shape, for example in a lid or a semi-rigid layer.
Dive deeper
On a laminating line the foil is bonded to paper, film or another substrate, and the bond quality depends on the surface staying clean and the web staying flat. A near pure web tends to sit smoothly against the substrate, so fewer air pockets and fewer wrinkles form at the nip, and the finished laminate looks and performs more consistently. Its low alloying content also keeps the finished laminate neutral when it is used close to food, which is often the deciding factor for a converter working on a sensitive product.
Where the alloyed grade wins is stiffness. If the laminate has to stand up on a shelf, hold a printed shape or survive a fold, a stiffer foil layer can carry the structure and allow a thinner substrate elsewhere, which can simplify the rest of the pack. That is a design decision rather than a rule, and the sensible approach is to test the laminate on the line before fixing the alloy, because adhesive, substrate and pressure all interact with the metal. Industry bodies such as the aluminium foil association Alufoil publish general background on how foil behaves in converting, which can help frame that trial. A short trial on your own line usually settles the question faster than any sheet.
How does each alloy behave in a container or a lid?
Containers and lids pull in opposite directions: one has to hold a shape, the other to release cleanly.
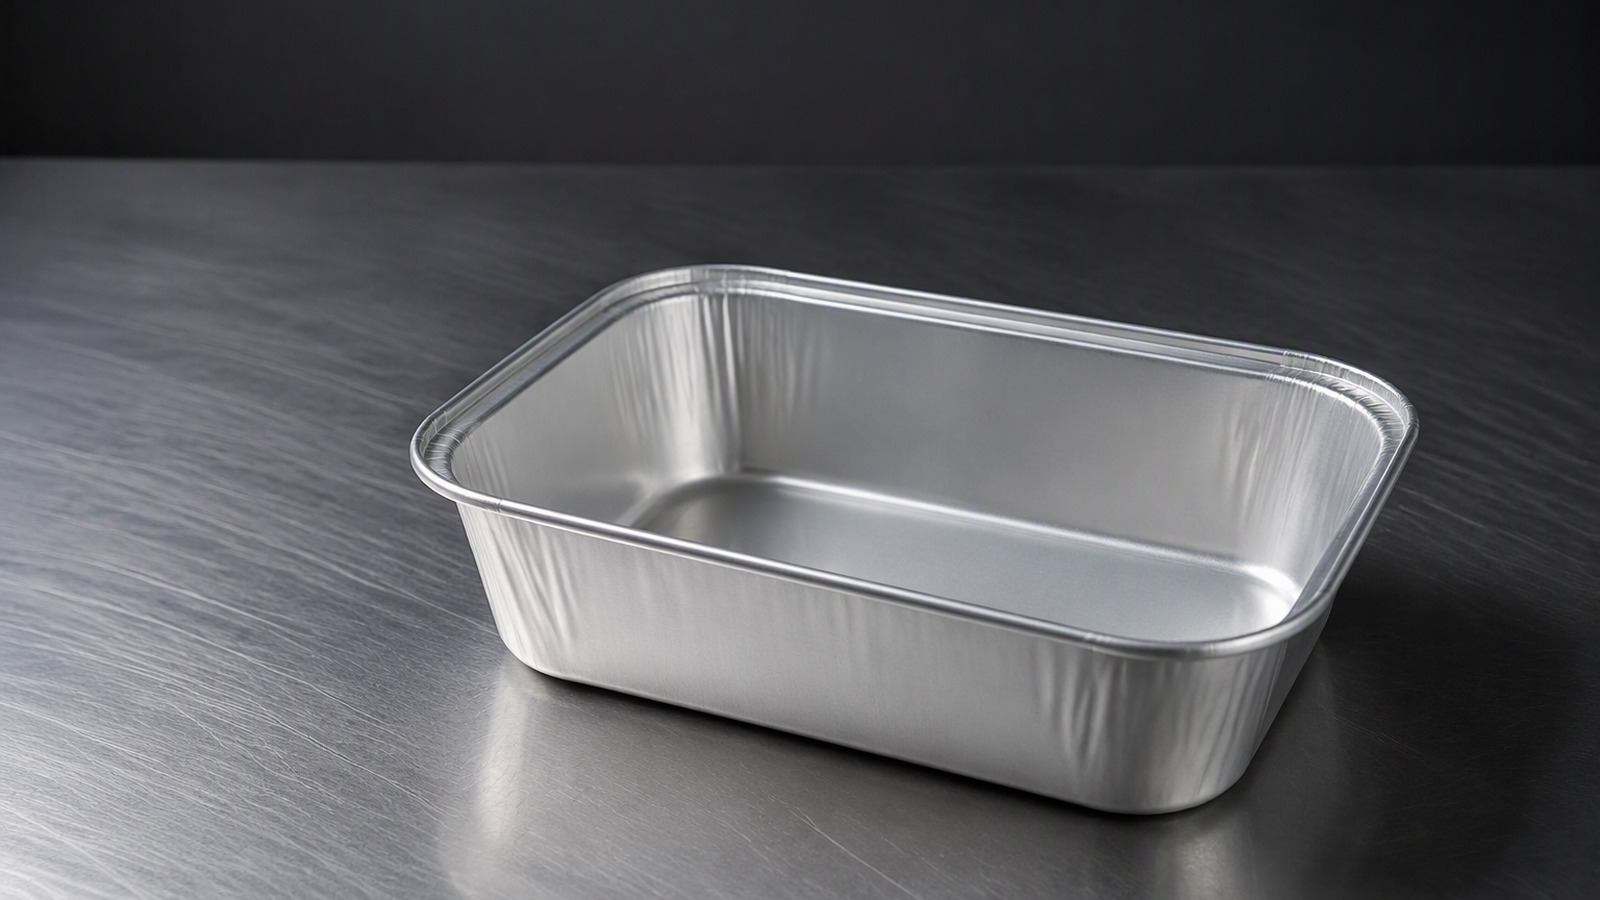
For a formed container or tray, 8011 is the natural choice because it resists the press and keeps its profile. For a lidding or lid film, 1235 is usually preferred because it seals and peels predictably over the filled pocket.
Dive deeper
A container is a forming problem. The foil is drawn or pressed into a die, and it has to stretch without tearing and then stay in the shape it was given through filling, sealing and transport. The stronger grade handles that better, which is why it is commonly supplied somewhere in the range from 0.005 to 0.20 mm depending on the depth and the stiffness the pack needs, with a core of 76 mm or 152 mm for the roll. A lid, by contrast, is a barrier and opening problem: it must sit flat over the container, seal around the rim and then peel away cleanly without shredding.
That difference explains why the same manufacturing plant can supply both grades to the same customer, sometimes on the same order. A catering pack might use an alloyed tray under a near pure lid, or the reverse, depending on which layer has to do the structural work and which has to do the sealing. Understanding the surrounding standards and terminology helps when specifying either part, and the European Aluminium industry association publishes explanatory material on foil products and their typical uses. In both cases the sealing surface and the drawing depth decide more than the alloy name.
How does the choice interact with temper?
Alloy and temper are two separate dials, and the second one often decides how the part behaves.
Temper sets how hard and springy the delivered foil is. The same 8011 supplied soft behaves quite differently from 8011 supplied hard, and a near pure grade is usually chosen in a soft state for laminating or lidding.
Dive deeper
Temper describes the amount of work the metal has been given, from fully soft states through to hard states such as O, H14, H16, H18, H22 and H24. A hard temper raises strength and stiffness but reduces ductility, so it suits flat webs and lidding where the foil should stay crisp and dimensionally stable. A softer temper bends and forms more easily, which suits deep draws and hand-formed shapes but offers less resistance to a press, so it can distort where the tool expects a firm web.
Because the two variables multiply each other, a buyer who fixes only the alloy has done half the work. A strong alloy in a soft temper may form more easily than the name suggests, while a nearly pure grade in a hard temper may feel stiffer than its chemistry implies. The practical rule is to describe the job rather than only the grade, so that the mill can propose a combination instead of a single value, and to test that combination on real equipment. General background on how the metal is rolled and finished is available from the aluminium industry association. A specification that names both values is far easier to quote than one that names only the alloy.
What should you put in an RFQ when the alloy is not fixed yet?
A good enquiry leaves the alloy open but pins down everything around it.
State the end use, the thickness window, the width and the temper, and say that the alloy is still open. Add the quantity and the destination port so the reply can cover both grades.
Dive deeper
An enquiry that names only an alloy is hard to answer well, because the mill has to guess at the application. An enquiry that describes the application, by contrast, lets the technical team propose the grade that suits it. Useful details include whether the foil is laminated, formed, lidded or wrapped; the thickness range you can accept, anywhere between 0.005 and 0.20 mm; the width you need, from 100 to 1500 mm; the temper you are considering, or the behaviour you need from the temper; and whether you need a 76 mm or 152 mm core.
It also helps to say how the foil will be packed and where it is going. A minimum order quantity of 3 MT per size is a common starting point, and stating the destination port, for example Qingdao, Tianjin or Shanghai, removes one round of questions. If thickness tolerance is one of your open questions, the note on aluminium foil thickness tolerance and yield explains the trade-offs before you commit. With those details in hand, a supplier can quote both grades side by side instead of asking you to choose blind.
Tell us the alloy, thickness, width and temper you need — our engineers will confirm feasibility and pricing.