Why Container Loading Planning Matters for Foil Importers
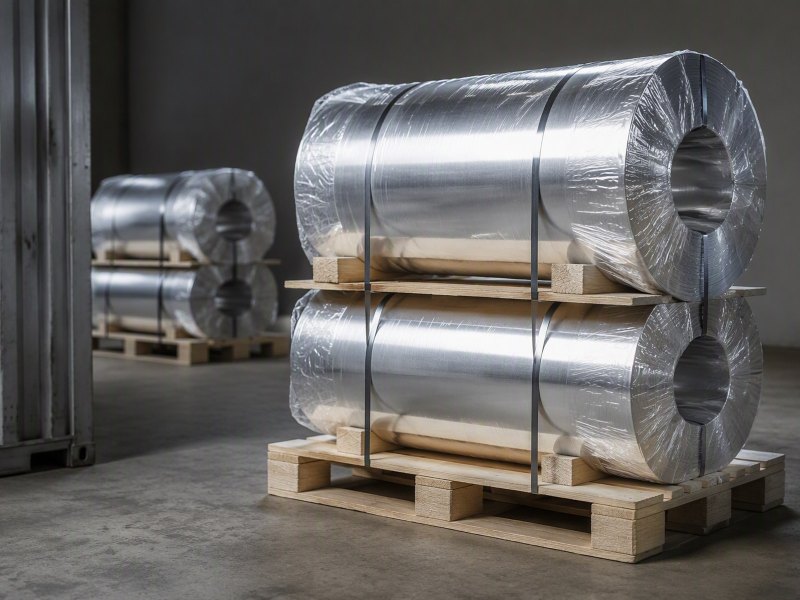
Foil is dense and easily damaged. A loading plan protects your material, your budget and your schedule.
Foil is dense and easily damaged. A loading plan protects your material, your budget and your schedule.
Aluminium foil is one of the densest packaging materials there is. A 20 ft container of jumbo reels can approach the road weight limit before the container looks full, which makes loading planning a commercial issue, not just a warehouse one. Three different risks meet in that plan: the weight your inland trucks may carry, the pressure the coils put on one another, and the moisture a long sea voyage invites.
Why does weight come before volume?
Mass, not floor area, is usually the first limit a foil shipment meets, so a plan built on cubic metres misreads the container.
Because foil is dense, the constraint is usually payload rather than cubic space. If a supplier plans by volume alone, you either ship an underweight container or discover the overweight problem at the port.
Dive deeper
Aluminium foil behaves unlike most packaging cargo because a jumbo reel concentrates a large mass into a compact cylinder. That density, described on Aluminium foil – Wikipedia, is what makes the payload limit bite long before the container looks full. Two full reels can occupy only a small part of the container floor yet account for a substantial share of the permitted road weight, leaving a great deal of unused space around them. A plan that counts cartons, pallet positions or cubic metres therefore misleads you from its first line.
The useful unit is mass per pallet position, checked against the road weight limit on the final inland leg rather than the container's nominal volume. Build the plan in three passes. List every reel with its alloy, thickness, width, temper and core, plus its gross weight, using aluminium foil roll data as your reference. Group the reels into pallet positions and add the pallet and packing weight, not only the metal. Then compare the total against the limit set by the truck, the chassis and the road rules between the port and your warehouse.
Hold back part of the payload as a safety margin, because packing-list weights are calculated while weighbridge weights are measured, and small differences are normal. A plan with no room for that difference may have to be unloaded or reworked at the gate.
How does coil orientation decide damage rates?
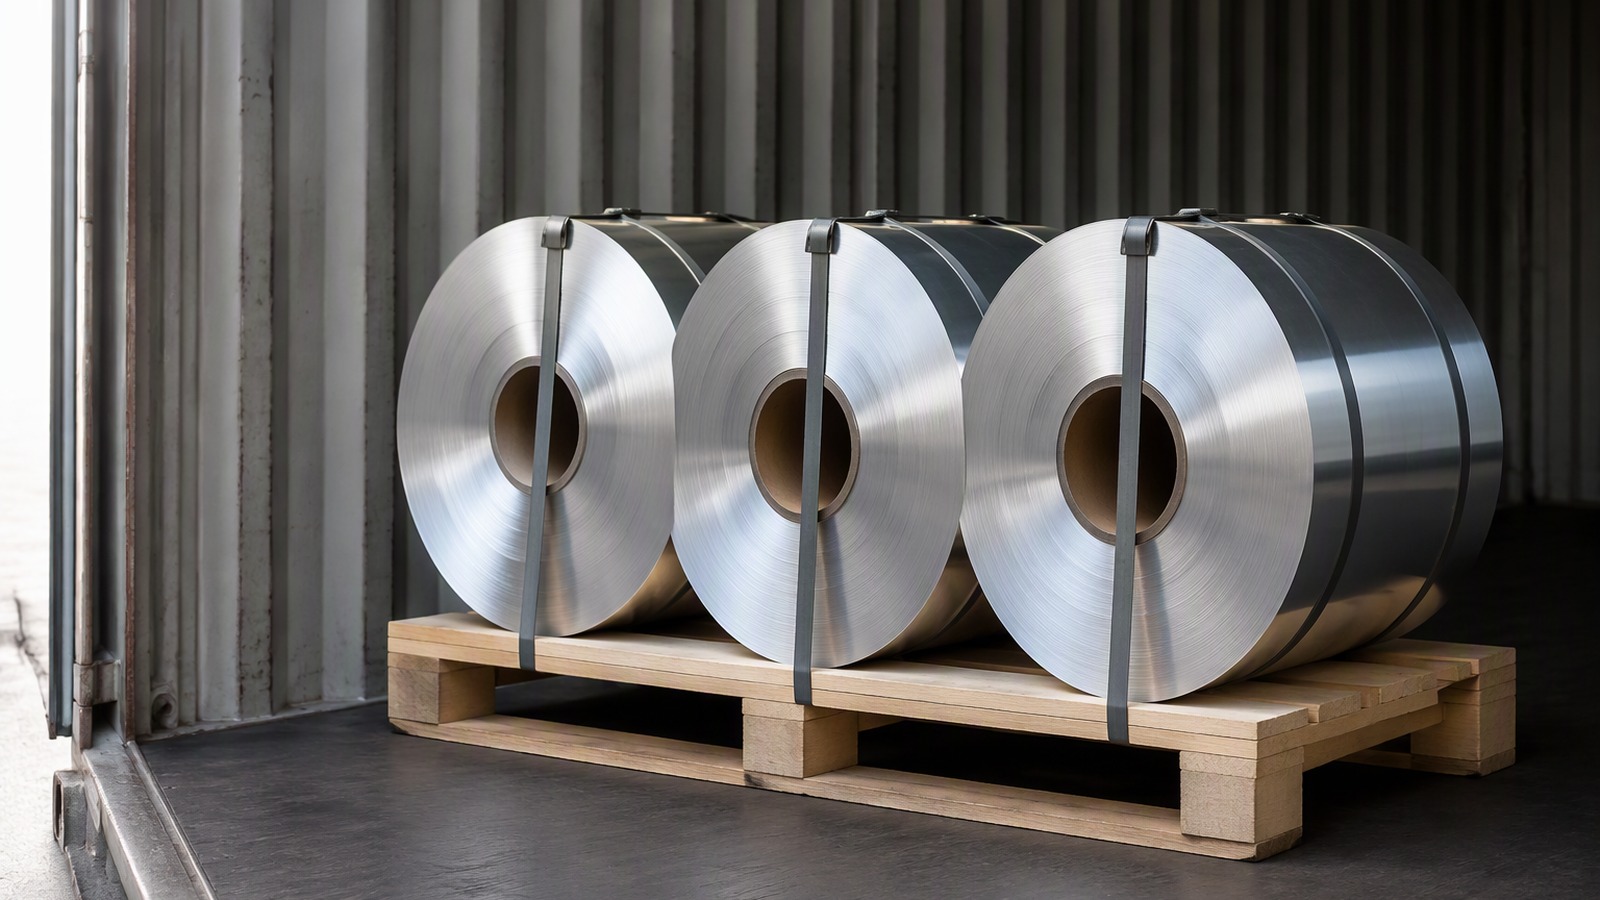
Orientation decides which part of a coil carries the load, and that single choice drives most transit damage.
Eye-to-sky pallets load more coils per container but put the coil edge in contact with the deck. Eye-to-wall pallets protect the edge and are the safer choice for thin gauge above 1,200 mm width.
Dive deeper
An eye-to-sky pallet stands a coil on its cut edge, so the full weight of the stack passes through a narrow ring of metal. One misplaced strap, a hard brake or a rough lift can bruise that edge, and an edge bruise is often visible only once the coil is unwound on your line. Eye-to-wall pallets lay the coil on its curved surface, spreading the load across a broad face and leaving the edge protected.
The trade-off is usually decided by gauge, width and journey length. Thin foil above 1,200 mm width and long ocean routes both favour eye-to-wall, while short regional moves of heavier gauge can accept eye-to-sky loading with little risk. Whichever you choose, ask for the coil to be strapped to a wooden pallet with corner protection, and record the orientation in the plan so the unloading crew repeats it.
Width tolerance and core diameter matter here as well, because a coil that sits unevenly on its pallet will lean against its neighbours. Reviewing how slitting width tolerance and core diameter are controlled helps you judge whether the pallet base will stay flat. Guidance from European Aluminium on handling rolled products is worth reading before you approve a loading method.
Why is humidity the quiet failure mode?
Moisture rarely announces itself at loading; it appears weeks later as surface staining that cannot be reversed.
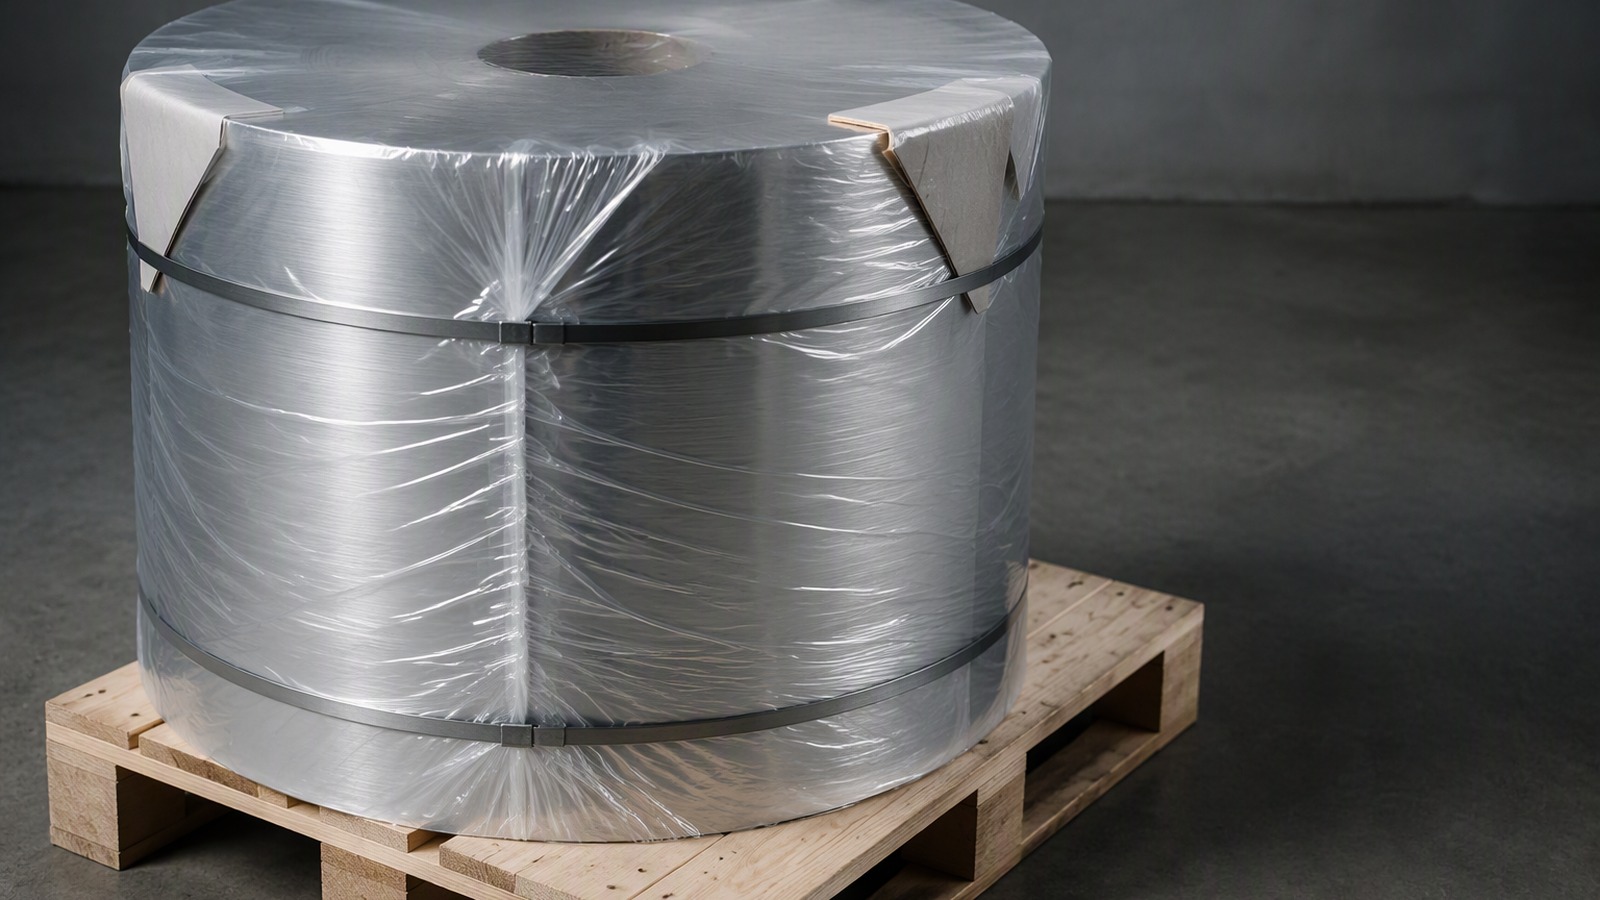
Foil can develop surface staining after a long sea voyage in a container that breathes. Moisture barrier wrapping, desiccant where appropriate and a documented inspection photo set before closing the doors are the practical controls.
Dive deeper
A container interior moves through temperature cycles as a ship crosses climate zones. Warm air holds moisture, and when the metal cools at night that moisture condenses on the coldest surface available, which is often the foil itself. The result is usually cosmetic rather than structural, yet cosmetic defects still trigger rejections, discounts and returned loads, and they are discovered by the buyer long after the loader has gone.
The practical defence is a sealed moisture barrier rather than a decorative wrap. Foil should leave the factory wrapped in barrier film with its edges protected and sitting on a wooden pallet so it never touches a wet floor. Where a voyage crosses several climate zones, desiccant is added inside the wrap, and the loading crew photographs the wrap, the straps and the doors before closing them.
Those photographs matter later because they show what left your supplier's floor. Our note on preventing water staining on aluminium foil explains the same controls from the mill side, while the European Aluminium Foil Association covers barrier principles for converted products. Add the wrapping step to your loading checklist and photograph it at the factory, so a later claim about staining never rests on memory.
What should you ask your supplier for?
Ask for the evidence that lets you check a loading plan before the container leaves the factory gate.
We issue these documents as standard for every export order.
Dive deeper
The documents you want are ordinary commercial paperwork, not special requests, and asking early costs nothing. A packing list should state alloy, temper, thickness, width, core, quantity and gross weight for each reel, because those figures are what your own loading model will use. A loading plan should show the layout, the orientation of each pallet and the order in which the coils were stowed.
Ask for the inspection evidence as well. A dated set of photographs taken before the doors close, showing the wrapped coils, the straps, the pallet bases and the container interior, gives you a record to compare against the container on arrival. If the load also carries aluminium foil container cartons, ask for that count separately, since trays and rolls rarely follow the same stacking rules.
Finally, confirm the parameters that shape the load: alloys such as 1050, 1060, 3003 or 8011, tempers from O through H24, thickness between 0.005 and 0.20 mm, width between 100 and 1500 mm, cores of 76 or 152 mm, and packing described as eye to sky or eye to wall on a wooden pallet with a moisture barrier wrap. This simply moves the paperwork forward, so the load can be verified while the container still stands at your supplier's floor.
How do you protect foil rolls from movement during transit?
A coil that can slide is a coil that will arrive bruised, so restraint matters as much as stacking.
Secure the load so no coil can shift: pack each pallet tight against its neighbours, brace the row against the container walls and keep heavy reels low, where movement is hardest.
Dive deeper
Movement is the enemy of a clean delivery, and it rarely acts alone. A coil that shifts by a few centimetres can lean on the next pallet, rub against a strapped neighbour or press its edge into a steel corner, and the damage may only surface when the coil is unwound. The forces at work are bigger than most people expect: a truck braking hard or a ship rolling in heavy weather turns a stationary stack into a load that wants to travel.
Three measures do most of the work. Fill the gaps between pallets with dunnage so the load is tight in every direction. Brace the first row against the container wall and the last against the doors, so the stack cannot move along the length of the box. And keep the heaviest reels low and toward the centre, because a low, centred mass both lowers the centre of gravity and is the hardest to shift.
Then check the details that fail quietly. Straps should pass over the coil, not across the unwound edge, and every strap should be checked by hand before the doors close. If the load mixes roll dimensions or includes converted packaging and container foil, plan the sequence so a light carton is never crushed by a heavy coil.
How do you load foil rolls so they unload faster at destination?
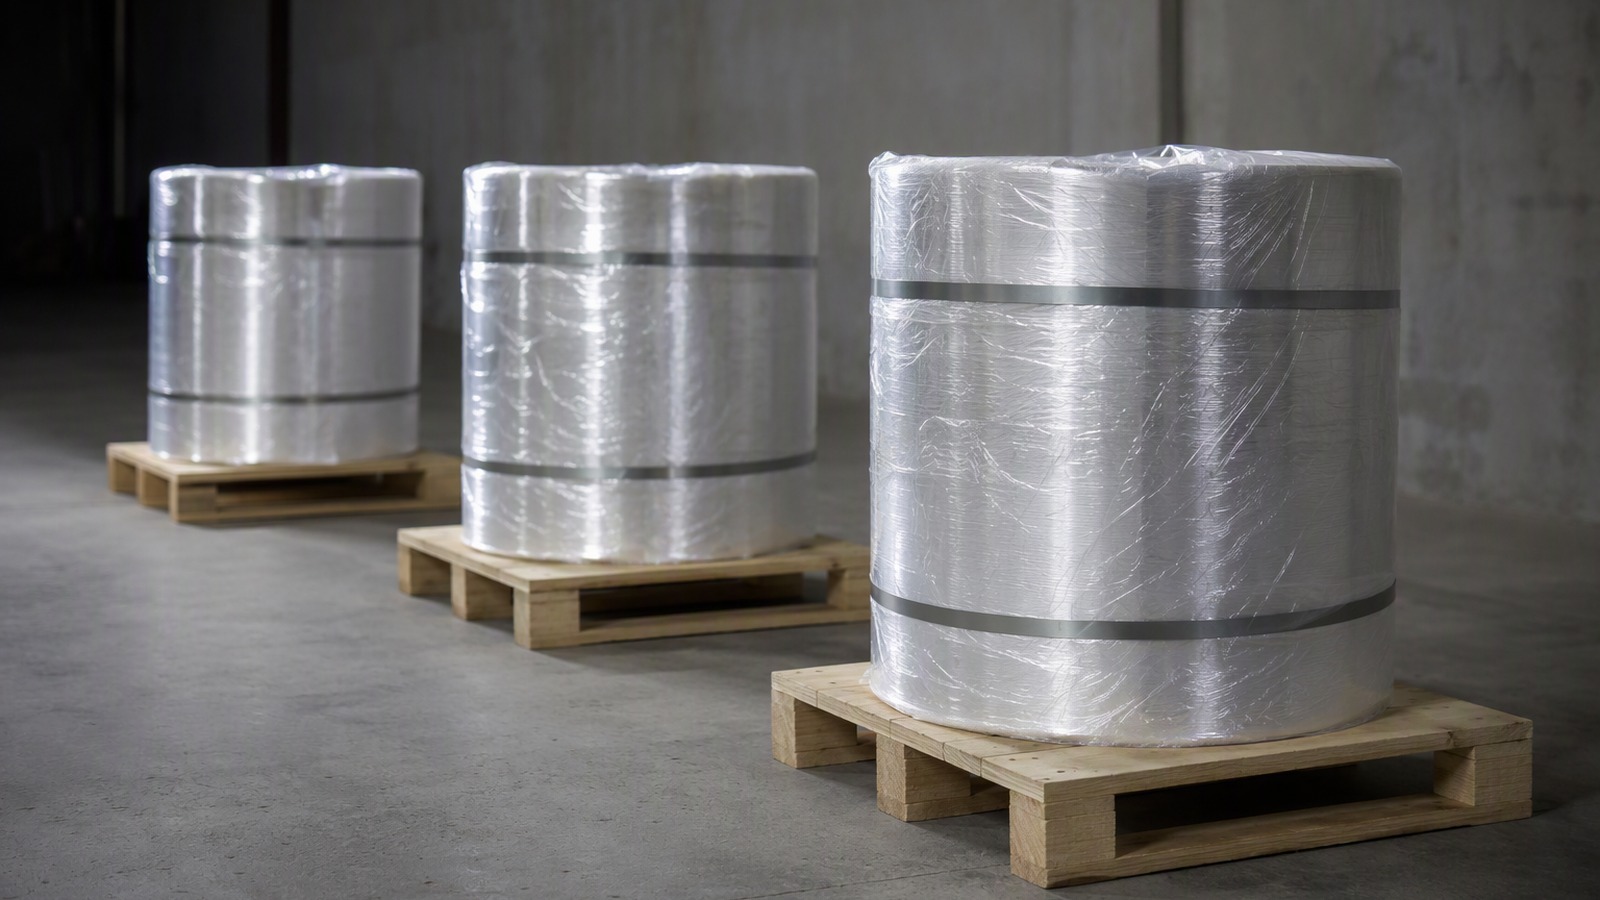
How you load decides how long the receiving crew spends at the door, and that time is part of your cost.
Sequence the load so the coils are opened in the order they will be needed: keep the first-needed pallets at the door end and avoid nesting a heavy reel behind a light carton.
Dive deeper
Unloading time is easy to overlook when the priority is fitting everything in, yet it directly affects demurrage, driver waiting time and the risk of damage from hurried handling. If the most needed reels sit at the far end of the container, behind pallets that must be moved first, the crew spends its energy shuffling the load rather than receiving it.
A simple sequence solves most of it. Place the pallets that leave first at the door end, keep the weight low and even, and make sure each pallet can be taken without lifting another. Where a load mixes rolls and trays, group the two so a forklift can pull a clean block instead of picking cartons out one by one.
Two documents make the difference here. A drawing that shows the stow sequence turns unloading into a routine, and a set of loading photographs answers the receiving crew's first question before it is asked. Weeks later, when a query arrives about a delivery, the same record lets you trace exactly how the load was built, which is often worth more than a hurried phone call. Label the door end clearly on the drawing, because a sketch the crew can read beats a verbal instruction shouted across a noisy yard.
How do you plan a mixed container of foil rolls and foil containers?
Mixed loads save freight but demand more planning, because rolls and trays behave very differently under load.
Keep dense rolls low and central, protect the lighter trays above and at the door end, and separate the two groups so nothing heavy can rest on a carton.
Dive deeper
Buyers often want rolls for converting and finished trays in the same shipment, and mixing the two can cut your freight spend. The catch is that a jumbo reel and a carton of tray stock have almost nothing in common as cargo. The reel is dense and rigid; the carton is light and crushes easily. Loaded carelessly, the heavy item wins, and the cartons arrive deformed.
Plan the mix by weight first. Dense rolls go on the floor, low and toward the centre, so they lower, rather than raise, the overall centre of gravity. Lighter cartons sit on top or at the door end, where they can be lifted without disturbing the rolls. Group each product so a forklift can take a complete block, and never let a carton sit under a reel, however briefly.
It also helps to label the two groups clearly and to note the mix on the loading plan. If your supplier both rolls the reels and converts foil into trays, a single plan can cover the whole order, and the tray cartons can be counted against the same shipment. Ask whether the same moisture-barrier packing protects both, because trays and rolls meet the voyage in different ways.
How does loading planning reduce damage claims and rework?
Most transit claims are decided by evidence, and a documented load is the cheapest evidence you can hold.
A clear loading plan, dated photographs and a packing list that matches the container turn a disputed claim into a short, factual exchange instead of a long argument.
Dive deeper
When a delivery arrives with a stained surface, a bruised edge or a crushed carton, the conversation quickly turns to where the damage happened. Without records, the answer is guesswork, and guesswork usually ends with a shared loss. With records, you can compare what left the factory against what arrived, and each party can see the same facts.
Planning also prevents rework. A load built to a written plan is easier to check, so mistakes such as a mismatched orientation or a missing strap are caught before the doors close rather than at the destination. That single check often removes the rework shift that would otherwise be needed to repack or rewrap a rejected delivery.
Finally, treat the plan as a living document. Keep the loading record with the shipment file, note any deviation on the day it happens, and review the plan after each delivery. General material guidance from The Aluminum Association can support your own internal procedure, and the same discipline that reduces claims also shortens the next negotiation. Keep the photographs, the plan and the packing list in one file, so whoever answers the claim has everything to hand.
Weight, orientation, moisture and paperwork decide whether a foil shipment arrives whole. Plan them together, document the load, and the container stops being a gamble.