Specifying Slit Width, Width Tolerance and Core Diameter
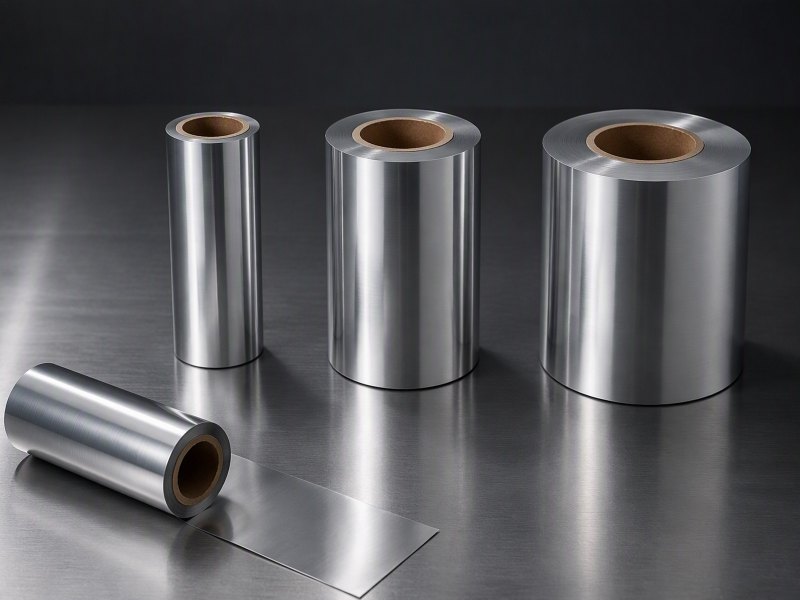
A width figure on its own is not a specification. Here is how slitting actually works, which tolerances are realistic, and how to write a width and core specification your line can accept without rework.
A width figure on its own is not a specification. Here is how slitting actually works, which tolerances are realistic, and how to write a width and core specification your line can accept without rework.
Most converting problems that get blamed on the mill trace back to an incomplete purchase specification. "300 mm wide" leaves out the tolerance, the core, the roll diameter and the winding, and every one of those can stop a line just as effectively as the wrong alloy. This is what to pin down.
How is slit foil actually produced?
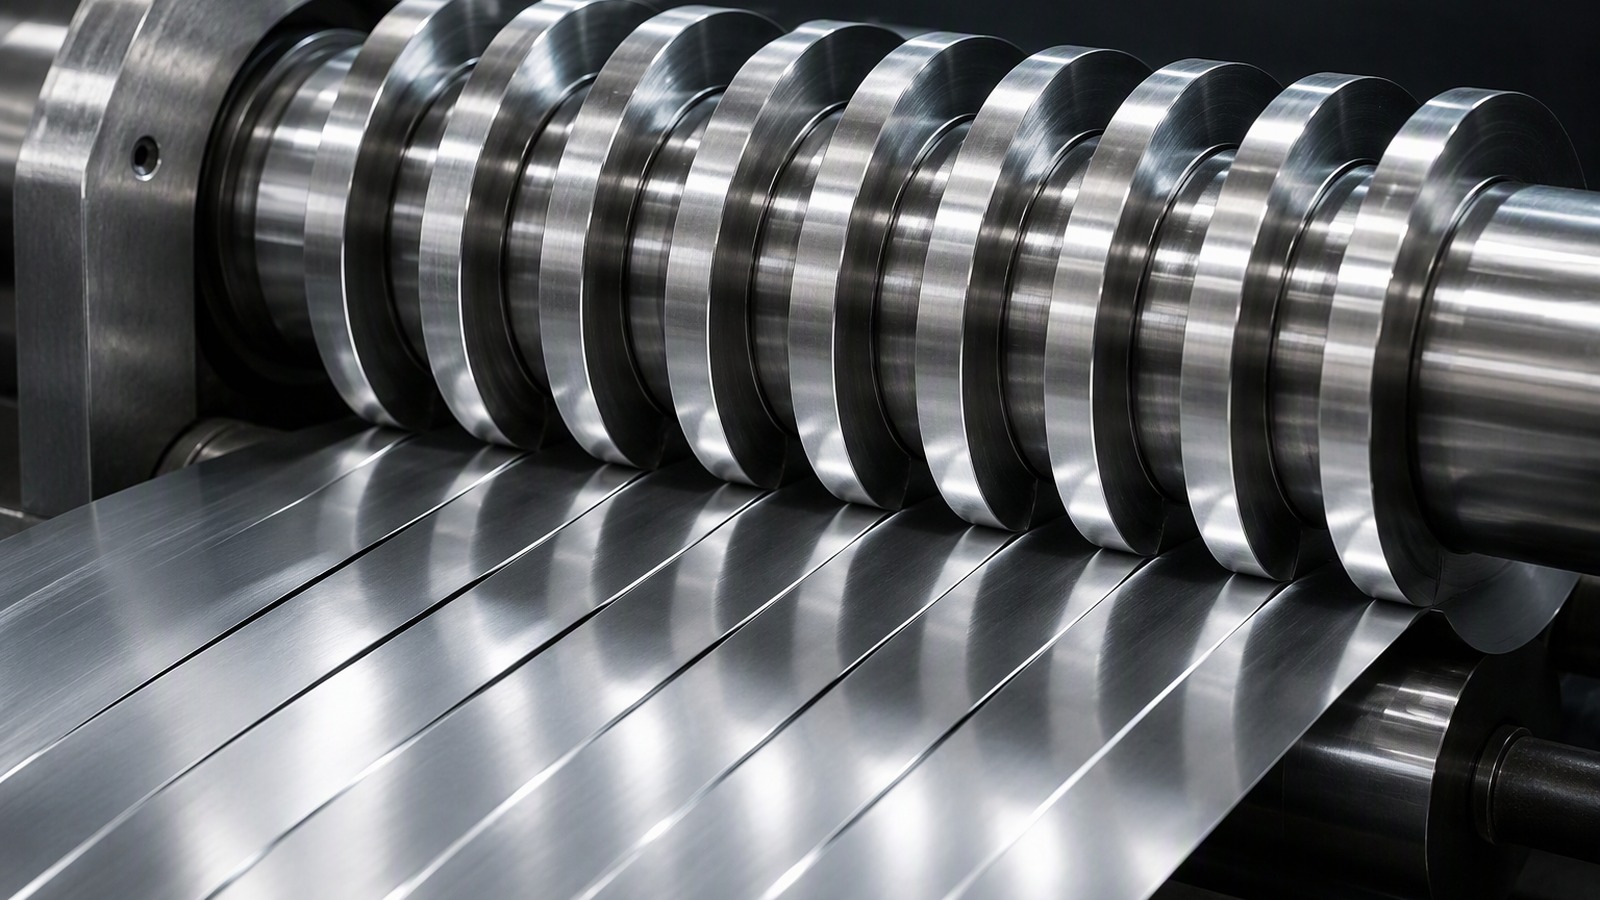
Foil arrives slit because a wide master coil is cut into narrower strips, so the width you receive is a cut edge rather than a rolled one.
Foil is rolled wide, then slit with circular knives and rewound onto cores. Every cut edge carries a little variation, coming from knife wear, web tension and knife position.
Dive deeper
Foil is rolled as a wide master coil. Slitting cuts that master into narrower strips with circular knives, then each strip is wound onto a core. The width you receive is therefore a cut edge, and any cut edge carries variation: knife wear, tension across the web, and the position of the knives all contribute. The tolerance band is not an admission of poor quality, it is a property of the process, and the sensible approach is to specify a band your line can genuinely tolerate rather than demanding a figure no mill can hold.
Where the variation enters
Three things move the edge. Knife wear changes the clearance between the upper and lower blades, so a worn set can push the cut away from nominal. Tension across the web pulls the strip sideways as it passes the knives, and uneven tension across a wide master shows up as a slight bow in a narrow strip. Knife position, meaning the setup of the whole slitting head, sets the nominal width itself, so a rushed changeover shows in the first metres of a new width. Because the three act together, the edge you measure is a result rather than a setting. Two rolls from the same master, cut on the same head, can sit at different points inside the same band. For background on the material itself, see the general description of aluminium foil.
What width tolerance is realistic, and how is slit width tolerance stated and measured?
A tolerance is only usable when it is written as a band around a nominal width and measured the same way at both ends of the order.
Standard commercial bands suit most converting, printing and packaging work. State the nominal width with a plus or minus band, then say exactly where and how the measurement is taken.
Dive deeper
Standard commercial tolerances are workable for most converting, printing and packaging operations. Tighter bands are achievable but expensive: they mean slower slitting, more frequent knife changes, more measurement and more scrap, and the cost lands in the tonne price. Before you insist on a tight tolerance, measure what your own process actually needs. If a two millimetre variation causes no jam and no visible defect, you are paying for control you will never see.
Stating it so that it can be checked
A usable statement has three parts: a nominal width, a band with a direction, and a place to measure. A band written as plus or minus is not the same as a band written as an upper limit only, and a line reading the drawing one way will reject a roll that was made the other way. The place matters as much as the number. A strip measured edge to edge includes any bow, while a strip measured at a fixed distance in from one edge does not. Say whether the reading is taken on the wound roll, on a length pulled off under tension, or both, and say how many positions along the length are checked, because one reading near the outer wrap says very little about the metres beneath it. For a broader picture of how foil is converted, see this industry overview.
Core diameter is a machine-fit question — why should it be agreed with the unwinder rather than assumed?
Because a core that does not match the mandrel stops the line before the first metre runs, and no width tolerance can rescue it.
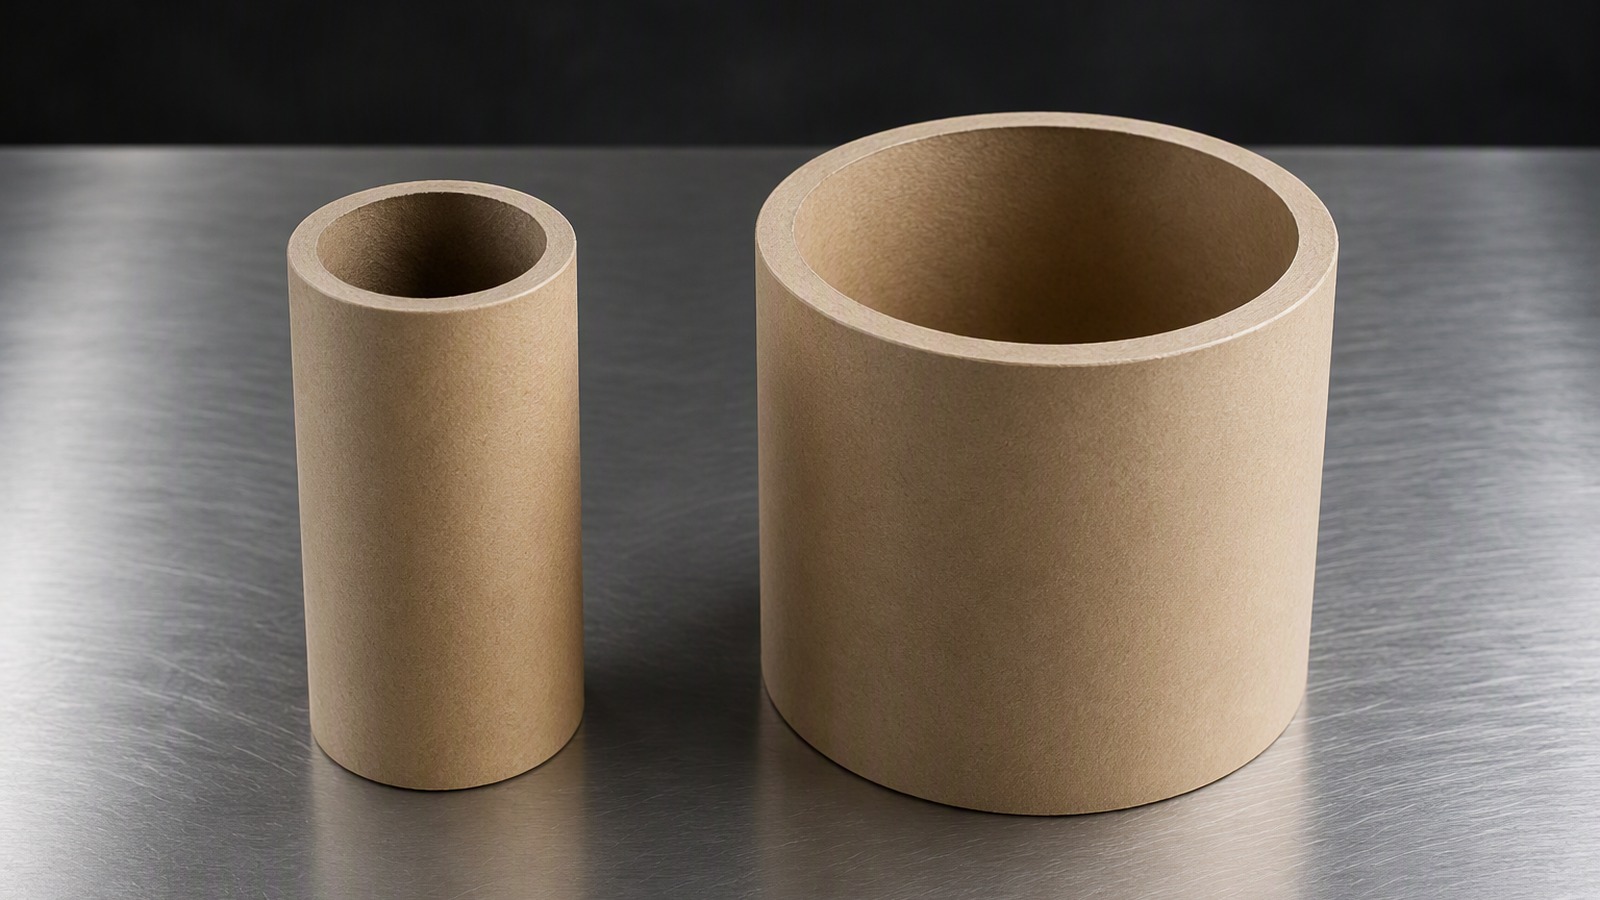
The core is defined by its inner diameter, and the unwinder is built around one size. Agreement means naming that size in the order instead of letting a default decide.
Dive deeper
Cores are specified by inner diameter, and the common sizes are 76 mm and 152 mm, with 38 mm used on smaller rolls. Getting this wrong is expensive in the least forgiving way: a roll that will not seat on your mandrel cannot be run at all. Confirm the core inner diameter your unwinder is built for, and specify it explicitly rather than assuming a default. If you operate more than one machine, record which core size each one takes.
What to check on the shaft
Agreement is a short conversation, but it has to happen before the order. Start at the unwinder: its mandrel or inflatable shaft takes one design bore, and an adapter is not always available for the size you assumed. Check whether the shaft grips the core from inside or holds it on end cones, because both arrangements need a clean, undamaged core edge to seat properly. Then check the take-up end, since a rewinder may take a different core from the unwinder. With a thin gauge such as 1235 aluminium foil, a core that fits loosely enough to slip will show as a tracking fault long before anyone inspects the core. A core size recorded on a machine card is more reliable than one remembered from an earlier order. Writing both numbers on the drawing is cheaper than reworking one roll.
How do roll diameter and weight decide how long a line can run?
They set the interval between roll changes, and both are capped by what your shaft, your lifting equipment and the container will accept.
Outer diameter and weight belong together: the same weight gives a different diameter at a different width, so state both and let the arithmetic be checked.
Dive deeper
Outer diameter determines how long the line can run between roll changes, and it is limited by winding stability. Larger rolls reduce changeover frequency but must still arrive undistorted in the container, which brings packing back into the picture. Tell the mill the maximum roll weight and diameter your handling equipment and shaft can accept, and tell it the minimum that makes a roll change acceptable to your operators.
Stating it as a window works better than stating a single target. Give a maximum, because the shaft, the lifting gear and the container each have limits that cannot be argued with. Give a minimum, because a light roll means frequent changes, and frequent changes cost more than the foil. Between the two, the mill can pick a length that suits its own winding without breaking your constraint. Remember that diameter and weight move together with width and thickness, so a figure copied from a narrower item may not translate. If one figure is unavoidable, make it a maximum and let the weight fall where it will, but expect a conversation about change frequency. Carry the same numbers onto the packing list, so the roll that leaves matches the roll that was specified. For wider context on how rolled aluminium products are handled downstream, see sector information on aluminium products.
Why do tension, edge quality and telescoping decide whether a roll runs?
Winding tension holds the wraps in line, so a roll wound with shifting layers arrives out of shape and will not track on your line.
Consistent tension keeps the cut edges flush. Where tension varies, wraps slide, the roll telescopes and the edges are already damaged before the roll reaches your unwinder.
Dive deeper
Winding tension determines whether the roll arrives as a usable cylinder or as a telescoped, edge-damaged coil. Consistent tension is what keeps the edges flush. If you have been receiving rolls with stepped or protruding edges, the conversation to have is about winding tension and packing, not just about the width figure.
Reading the symptoms
Damage tells you where to look. A roll that telescopes has been wound too soft near the outside, or has been handled by the outer wrap instead of the core. Stepped edges on one side only usually point to a tension profile across the width rather than to the knives. Bruised or folded edges suggest packing and transit rather than winding, especially where the damage is local and matches a strapping position. None of these faults is fixed by narrowing the width tolerance, which is why an argument about the width figure rarely settles a complaint about edges. If the outer wraps are unusable, the practical question becomes how much of the roll you can still run, and whether a heavier winding pattern on the next order would cost less than the waste. The place to start is the aluminium foil roll specification itself: width, core and roll weight written together give the winder something to work to.
When is traverse winding for automated lines the right choice?
When the line must run without stopping for a roll change and the foil has to be fed continuously from a spool rather than a plain roll.
Traverse winding suits automated and high-speed lines that need continuous feed, and it needs its own specification because spool dimensions and winding pattern cannot be improvised afterwards.
Dive deeper
Automated and high-speed lines often need spooled or traverse-wound material rather than a plain wound roll, so the foil can be fed continuously. The requirements are more specific: spool dimensions, bore, winding pattern, and often a limit on splices or a maximum length per spool. Specify these before the order, because converting a wound roll into a spooled package afterwards is not always possible.
What changes on the line
A spool feeds from the side, so the spool body, its bore and the way it sits on a chuck all become part of the machine interface, just as the core does on a plain roll. The winding pattern controls how the foil leaves the package: too coarse and the material pays off in steps, too fine and the layers press on each other. Splices matter more than on a plain roll because an automated line may not tolerate a stop at all, which makes both the number of splices and their position worth agreeing in advance. Length per spool then sets how often an operator intervenes, and that figure is easier to fix from your line speed than from a catalogue. Where spooled material is not yet justified, an ordinary roll remains the simpler package; industry resources on foil converting, such as this foil industry resource, are a reasonable starting point for the comparison.
What happens downstream when the slit width drifts?
The strip stops sitting where the guides expect it, and the line starts correcting for a fault that was built in at the slitter.
Drift shows up as tracking error, folded or bruised edges, register loss on print and occasional web breaks. It is usually blamed on the machine long after the roll was slit.
Dive deeper
Width drift is quiet, which is what makes it expensive. Nothing fails at the moment the strip is a fraction of a millimetre outside its band; the guides simply work harder, and the operator compensates, and the run continues. The cost appears later as a rejected print job, a jam at a folding station, or a length of coated material that has to be cut off. Narrow strips amplify the effect, because the same absolute deviation is a larger share of a narrow width, and a bow that is invisible on a wide master can steer a narrow strip off its path entirely.
There is also a stacking effect. A line tuned to one width runs a slightly different width badly, and the correction an operator dials in stays in place for the next roll. Over a shift, the machine can end up set for a roll that no longer exists. The way to break that chain is to record the width actually measured on arrival, not the width ordered, and to compare the two. Where the downstream process is sensitive to gauge as well as width, it is worth reading thickness tolerance and yield alongside this article, because the two variations often arrive together. To see how a master becomes a narrow roll, how a jumbo roll becomes a slit roll follows the same material through the slitter.
What does a complete width and core specification look like, and what goes into the order so both are unambiguous?
It names the width, its band, the core, the roll weight and the winding, and it says how each of those will be checked on arrival.
Put the nominal width with a plus or minus band, the core inner diameter, the roll weight window, the outer diameter and the winding type into the order, then confirm what is achievable before the price is fixed.
Dive deeper
Width, tolerance and core are everyday requirements for us. Tell us the slit width and its tolerance, the core inner diameter and the roll weight your equipment accepts, and we will confirm the achievable specification before quoting. See our foil roll and flat sheet range, or aluminium foil sheet where flat cut material suits you better than a roll.
A specification that survives the journey is short and boring. It gives the alloy and temper, the thickness, the slit width with its band, the core inner diameter, the acceptable roll weight window, the outer diameter and the winding. It also says which of those are fixed requirements and which may be adjusted if something has to give, because a mill that has to guess which line is negotiable will guess wrong. Add the packing method, since a roll that arrives dented fails the same test as a roll that is the wrong width. Finally, write down how arrival will be checked: what is measured, on what, and by whom. Two people measuring the same roll in different ways will disagree, and that disagreement is easier to settle before the first container than after it.
Width, tolerance and core are one specification, not three separate wishes. Write the band, the core size and the roll weight together and the roll arrives ready to run.