How to Choose the Right Aluminium Foil Thickness
Thickness decides strength, barrier performance and cost. Here is how to match gauge to your application instead of over-specifying.
Thickness decides strength, barrier performance and cost. Here is how to match gauge to your application instead of over-specifying.
Aluminium foil is specified in micrometres, and a few micrometres change both the performance and the price of the finished pack. Buyers who over-specify pay for material they do not need; buyers who under-specify get pinholes and complaints.
Should you start from the barrier requirement?
For moisture and oxygen barrier in flexible packaging, the foil layer is what does the work.
Below roughly 9 µm, pinhole counts rise sharply after lamination unless the foil is handled carefully, so most pouch structures sit between 9 µm and 12 µm.
Dive deeper
Barrier performance is not a single number. Water vapour transmission and oxygen transmission both fall as the foil layer gets thicker, but they fall along a curve rather than a straight line. Once the metal layer is continuous and free of through-thickness defects, adding another micrometre buys very little extra protection and simply adds cost and weight to the pack.
That is why the practical advice is to pick the thinnest gauge that still laminates cleanly, then protect it during handling. The aluminium foil thickness of the plies around it matters too: a biaxially oriented film on each side carries most of the mechanical abuse while the foil does the barrier work. If a converter can run a 9 µm web without creasing, that structure usually outperforms a heavier, clumsier one.
Consider what the pack actually faces. A dry snack needs a moisture barrier, a coffee pack needs oxygen and aroma control, and a retort pouch needs the foil to survive heat and pressure. Each case shifts the point at which extra thickness stops paying. When a customer asks for a heavy gauge just to be safe, ask which failure they are trying to prevent. If nobody can name a failure mode, the extra micrometres are insurance against nothing. The Aluminium foil - Wikipedia article is a useful primer on how thin rolled metal achieves its barrier.
Should you then consider mechanical load?
Container and tray foil is not chosen for barrier at all — it is chosen for formability and rigidity.
Trays deeper than 40 mm typically need 60 µm and above, while lidding stock works well between 30 µm and 50 µm.
Dive deeper
Once a pack is formed, the foil itself becomes the structure. Deep drawn trays fail in three ways: the wall thins until it perforates, the corner cracks, or the flange loses flatness and will not seal. All three are driven by gauge, and all three get worse as the draw ratio rises.
That is why the 0.07 mm container gauge that appears in so many tray specifications is a compromise. It draws to a useful depth without thinning to the point of perforation, and it still holds a flange flat enough for a heat seal. Our 3004 container foil is a typical choice for this duty, because the alloy gives a good balance of strength and forming behaviour. Going thinner saves material on every tray, but the reject rate at the forming press usually rises faster than the metal saved.
Lidding is a different job again. A lid has to peel or cut cleanly, sit flat on the flange and resist puncturing by a fork, and none of those require deep drawing. That is why lidding stock can sit at 30 µm to 50 µm while a tray wall sits above 60 µm. The European Aluminium association publishes useful background on how these applications are specified across the industry.
Should you then consider the converting process?
Printing, coating and heat sealing all apply tension.
A foil that is too thin will stretch and register poorly; a foil that is too thick will not form cleanly around tight radii.
Dive deeper
The converting line is where an otherwise sensible gauge choice either works or fails. Web tension, roller alignment and temperature all interact with thickness, and a change of a few micrometres can move a job from comfortable to marginal.
On a press, thinner foil stretches more under the same tension, so registration drifts between stations. Converters compensate with lower tension and better web steering, but there is a limit. On a laminator, a thicker foil carries more stiffness into the nip, which can lift the edges and trap air. On a heat sealer, thickness sets how much energy reaches the seal layer before the foil conducts it away.
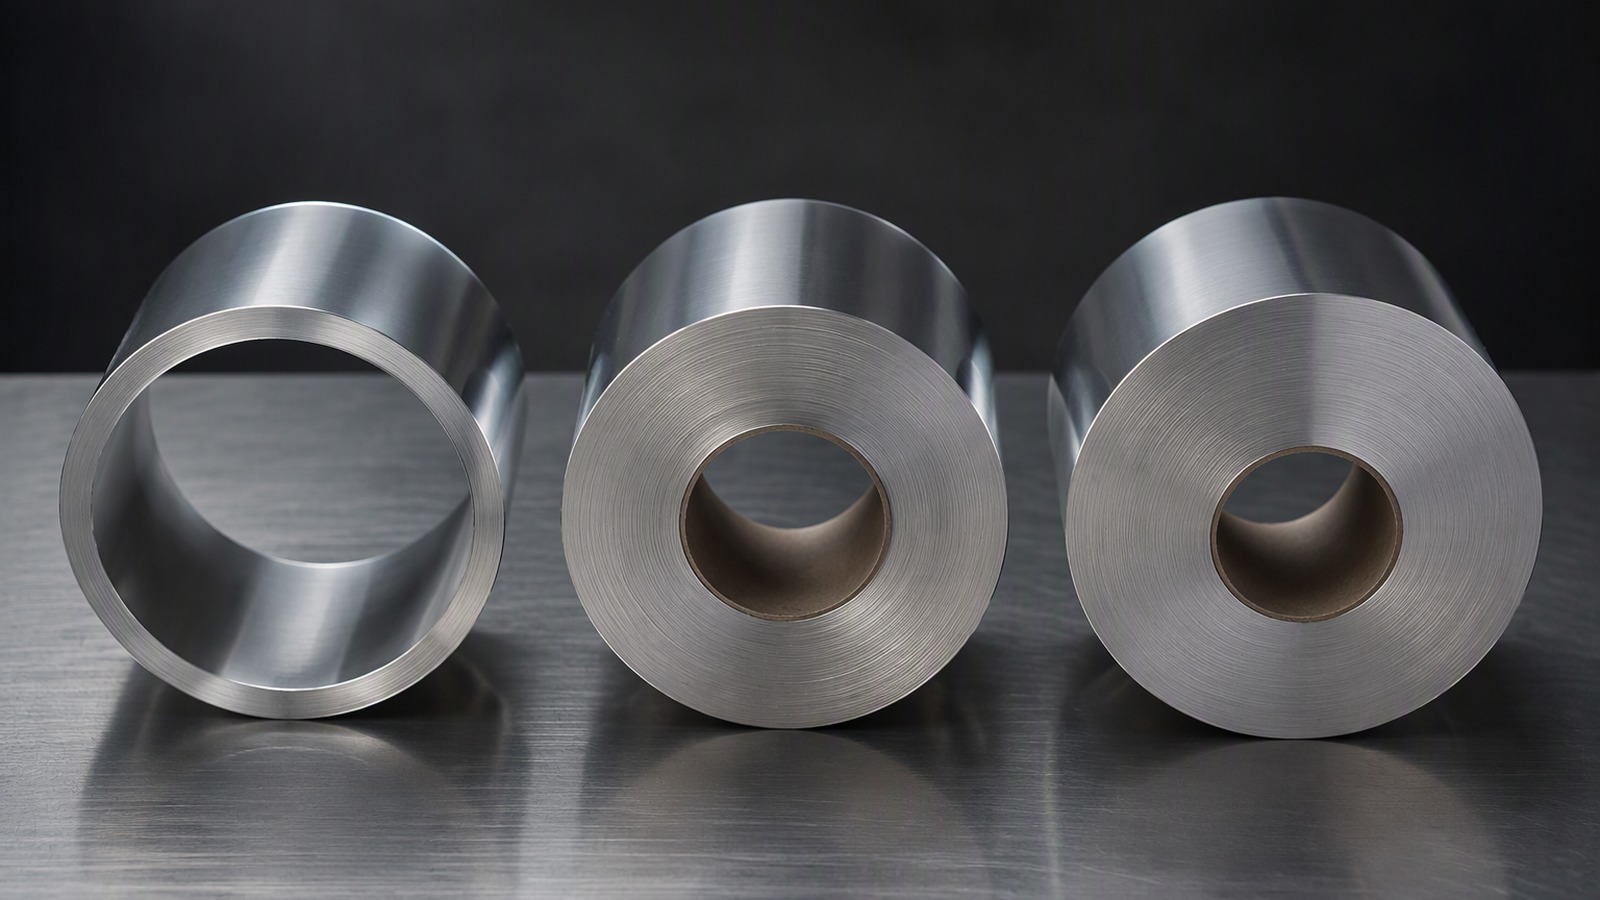
The wider message is that gauge should be chosen together with the process, not before it. A supplier who only quotes a thickness has answered half the question. The foil roll and sheet range we manufacture is rolled to standard widths and cores so that converters can plan a run without special tooling, and the reference material from the National Institute of Standards and Technology explains the measurement side of the same problem.
Confirm the running tension the press will use, the maximum line speed and whether the foil is printed, laminated or coated in the same pass. Ask the converter to name the tightest radii and the smallest repeat on the job. Where the web is also slit or rewound, roll quality matters as much as the gauge, because a soft edge or a loose wind creates the very creases that thin foil cannot tolerate.
Is there a practical starting point?
Send us your end use and we will confirm a workable gauge window, including the tolerance we can hold on the rolling mill.
Bring the application, the pack format and the converting line; those three inputs usually narrow the choice to a short list of gauges.
Dive deeper
A starting point is useful because it removes the two most expensive mistakes: ordering far more metal than the job needs, and ordering a gauge that the line cannot handle at speed. Neither mistake shows up in a quotation, and both show up in production.
Work through the questions in this order and the answer usually falls out on its own. First, name the barrier the pack has to hold. Second, decide whether the foil is a flat lidding layer or a formed tray wall. Third, check what the press, laminator and sealer can actually run. Only then look at price per tonne, because a cheap gauge that raises the reject rate is never cheap. Thickness control interacts directly with yield, as our note on aluminium foil thickness tolerance explains.
When a specification is still open, it also helps to compare the gauge you are considering against the published range for the alloy. Thickness from 0.005 mm to 0.20 mm covers everything from ultra-thin packaging plies to heavy tray stock, so there is normally no reason to invent a non-standard figure. If a mill can hold a window rather than a single value, the converter gains the freedom to run slightly heavier or lighter as the job demands.
How do pinholes influence the gauge you specify?
A pinhole is a pathway, and one pathway defeats a barrier no matter how heavy the rest of the web is.
Pinhole counts fall steeply as gauge rises, which is why thin gauges are judged on their handling as much as on their thickness.
Dive deeper
Pinholes do not all have the same cause. Some are rolled into the strip as the metal passes through the mill; others are opened later on the converting line when a thin web creases, drags over a sharp edge or releases trapped air. The first kind is a mill quality issue, the second is a handling issue, and they need different responses.
What matters commercially is the count per unit area that survives into the finished pack. A web with a high starting count can still be used if the lamination bridges the holes, but the margin is thin. This is why the same nominal gauge behaves differently in two plants: one runs clean, controlled tension and the other does not.
When a pack fails on barrier, the foil is often blamed before the process is checked. It is worth separating the two. Our explanation of what causes pinholes in thin aluminium foil goes through the common mechanisms in order, and the standards work of ASTM Committee B07 on Light Metals and Alloys covers the test methods behind them.
Ask the mill for the inspection basis, not just a pass or fail statement. Confirm how the count is sampled across the width, what the smallest detectable hole is and whether the report covers the full coil. On receipt, unwind a few metres and look for bright pinpricks against a dark background. Compare the incoming coil against the one it replaces before releasing it to the line.
How much does thickness tolerance matter?
A nominal gauge is a target, and what the line actually feels is the tolerance band around it.
A tight, honest tolerance is worth more than a slightly thinner nominal figure, because the process has to cope with both edges of the band.
Dive deeper
Tolerance describes how far a delivered coil may sit above or below its nominal thickness. On a rolling mill it is the difference between a specification that is easy to hit and one that demands constant adjustment. On the converting line it decides how wide a window the operator has before registration drifts or a seal weakens.
Buyers often compare only the headline gauge and ignore the band, which is a mistake. Two suppliers quoting 30 µm can deliver very different material: one holds a narrow spread around the target, the other a wide one. Over a long run, the narrow supplier gives a more stable yield even if the average thickness is the same.
There is also a commercial angle. Rolling to a tighter tolerance costs more because more of the output is checked and more of it is rerolled, so the price per tonne moves with the band you ask for. The right question is not how tight a tolerance is available but how tight the application genuinely needs. Most packaging jobs are comfortable with a normal commercial band; only a few demand the tightest.
Ask how the band is verified as well. Two coils can share a nominal figure and still behave differently if one is measured at the edges and the other across the full width. It also helps to know whether the tolerance is written as a percentage or an absolute value, because the two tighten at different rates as the gauge rises.
Does alloy or temper affect the thickness you choose?
Thickness and metallurgy are chosen together, because a stronger alloy can sometimes do the same job with less metal.
Alloy and temper set how the foil behaves at a given gauge, so they are part of the same decision rather than a separate one.
Dive deeper
Not all foil of the same thickness forms in the same way. The common packaging and container grades are 1050, 1060, 1100 and 1235 for general work, 3003 and 3004 for formed applications, and 8011, 8021 and 8079 for specialised packaging where barrier and surface quality matter. Each behaves differently when it is drawn, folded or sealed.
Temper matters just as much. Fully soft O material forms easily but lacks stiffness, while the work-hardened tempers such as H14, H16, H18, H22 and H24 trade some formability for strength and flatness. A tray that cracks at 60 µm in a soft temper may form cleanly at the same gauge in a stronger one, and the reverse is true for deep draws that need the metal to flow.
The practical consequence is that gauge and metallurgy should be specified as a pair. Choosing a thickness without naming an alloy and temper leaves the supplier to guess, and a guess that satisfies the thickness number may still fail at the press. It also explains why the same application can be quoted at slightly different thicknesses by different suppliers without either being wrong.
When a supplier proposes an alternative, ask which property is doing the work in the new combination and whether the forming station has run it before. Mechanical properties move with temper even at a fixed thickness, so a substitution that looks equivalent on paper can still change how the metal flows in the die.
How should you compare gauge against cost?
Every extra micrometre is paid for on every square metre you convert, so gauge is a cost decision as much as a technical one.
The cheapest foil is the thinnest one that still passes the pack, the line and the customer, and that is where the comparison should start.
Dive deeper
Foil is bought by weight and used by area, so the two measures pull in opposite directions. A thinner gauge spreads a tonne of metal over a larger area, which lowers the cost of each pack, but it also raises the risk of a failure that costs far more than the metal saved. The balance point is application specific.
It also helps to compare like for like across the whole order rather than the header price alone. Widths from 100 mm to 1500 mm and bores of 76 mm or 152 mm change how efficiently a coil runs on a given line, and a gauge that suits one width may waste material at another. Packing matters too: eye to sky or eye to wall on a wooden pallet with a moisture barrier wrap protects the coil in transit. The minimum order of 3 MT per size exists because small lots on a rolling mill carry disproportionate setup cost, and shipments typically move through Qingdao, Tianjin or Shanghai.
Finally, be wary of a quotation that answers only the gauge question. The useful comparison is a workable thickness window, a stated tolerance and a coil format your line can run, priced together.
Match the gauge to the barrier, the load and the line, then hold a sensible tolerance around it. The thinnest foil that reliably passes the pack usually wins.