What Causes Pinholes in Thin Aluminium Foil?
A guide for packaging engineers, buyers and quality teams: what causes pinholes in thin aluminium foil, how gauge, alloy and rolling practice control them, why they matter for barrier performance, and how to state an acceptance approach.
A tiny light speck on a backlit foil roll can fail an entire pharmaceutical or food packaging run, so buyers and quality teams cannot afford to treat pinholes as cosmetic.
The direct answer: pinholes in thin aluminium foil come from the way gauge, alloy and rolling practice interact - very thin gauges, hard or coarse second-phase particles, and unstable reduction leave tiny perforations. Their importance depends on the barrier duty, so the acceptance approach is agreed to the application.
Yield is not the only thing at stake here, and neither is appearance. The sections below take the questions buyers, packaging engineers and quality teams raise most often, from the metallurgy of a perforation to how a specification should word acceptance and how received material is checked.
Why do thin gauges produce more pinholes than heavy foil?
Pinholes are a function of gauge first. As foil gets thinner, the population of tiny perforations rises, because less metal has to span the same random defects.
Thinner foil carries more pinholes because the reduction leaves less material to close or cover small inclusions, scratches and roll marks. Barrier duty, not gauge alone, decides whether that matters for a given pack.
Dive deeper
Gauge is the strongest single driver. Foil is rolled to thicknesses from 0.005 mm to 0.20 mm, and the lower end of that range is where perforations become a routine topic. Each further reduction pass thins the web and stretches any non-uniformity, so a small hard particle, a scratch from a roll, or a sliver of oxide that would sit harmlessly inside a much heavier sheet can become a through-hole once the same feature is drawn down to a few thousandths of a millimetre. The mechanism is geometric: a pinhole is a hole whose diameter is comparable to the strip thickness, so as thickness falls, the same physical flaw spans a larger fraction of the section and is more likely to cross it entirely. That is why the relationship between gauge and pinhole population is not linear - it steepens.
A second reason is that thin foil is often rolled in a double layer, with the two sheets separated afterwards. Double rolling improves productivity and the surface of the outer face, but the mating faces can trap third bodies between them. Those trapped particles imprint both sheets, and on the thinner product the imprint is more likely to become an open perforation. Web tension, flatness and roll-surface condition therefore matter more at low gauges than at high ones, because there is less metal to absorb a local disturbance.
Reading gauge against barrier duty
Gauge alone does not decide acceptability. A pack that only blocks light or dust tolerates far more perforations than one that must hold a sterile or oxygen-sensitive product. The useful question is therefore not how many pinholes could be allowed in general, but how much barrier this application can afford to lose. Downstream, that judgement links directly to thickness tolerance and yield: a strip that sits at the thin end of its tolerance band for the whole coil behaves like a thinner foil and will carry the pinhole population of a thinner foil. Buyers who track gauge control and perforation results together see the effect early. General background on the material and its rolling history is set out in Aluminium foil - Wikipedia, and the practical link between gauge control and usable output is discussed in our note on thickness tolerance and yield in aluminium foil rolling.
How does alloy and temper choice affect pinhole formation?
Alloy and temper set the metal's strength and cleanliness, and both change how a thin web behaves as it is reduced and handled.
Cleaner, softer alloys roll with fewer through-holes, while hard tempers resist handling damage but can crack at low gauges. Alloys such as 1050, 1235, 8011 and 8079 are common in thin packaging foil.
Dive deeper
Alloy selection changes two things that matter for pinholes: the amount and character of second-phase particles, and the work-hardening behaviour of the matrix. Particles and inclusions larger than the local strip thickness are natural initiators, because the metal cannot flow around them smoothly during rolling; instead the particle either fractures or creates a void beside it, and that void can open through the sheet. Alloys formulated for foil - among them 1050, 1060, 1100, 1235, 3003, 3004, 8011, 8021 and 8079 - differ in how much coarse constituent they carry. The leaner 1xxx grades such as 1050 and 1235 are chosen when surface and perforation quality dominate, while the higher-strength 8xxx and 3xxx grades are chosen when the pack needs stiffness or formability and the converter accepts a different balance.
Temper plays the complementary role. Soft tempers such as O let the web deform plastically without cracking, which helps it roll down to fine gauges, but a very soft foil dents and creases easily in later handling. Harder tempers such as H18 or H22 hold their shape and resist handling marks, yet at very low thickness a hard, low-ductility strip is more prone to edge cracking and to localised fracture around a flaw. The choice is therefore a balance, and it is set by the application, not by a universal rule. Tempers such as O, H14, H16, H18, H22 and H24 can be specified against a defined end use.
Why converters often choose 8079
For thin, barrier-critical packaging, 8079 is widely used because it combines good rolling behaviour at low gauge with a fine, well-controlled microstructure. The result is a foil that can be drawn to fine thickness while keeping perforations under control, which matters for laminates that must resist moisture and oxygen. A representative thin product is thin aluminium foil 8079 at 0.009 mm gauge, supplied in the tempers and widths that downstream laminators and printers require. The point is not that one alloy is universally superior, but that matching alloy and temper to the planned gauge and to the barrier target is the first lever a buyer controls.
What happens during rolling that opens a pinhole?
Rolling practice decides how many potential flaws become real holes: reduction schedule, roll condition, tension and cleanliness all leave their signature in the web.
A pinhole opens when a rolling flaw crosses the strip - an imprinted particle, a roll-surface mark, an oxide sliver, a tension spike or a fold that is later thinned. Stable, clean rolling keeps that population low.
Dive deeper
Rolling is a sequence of controlled deformations, and a defect becomes a pinhole only if it survives the whole sequence. Four practice variables dominate. The first is the reduction schedule: how the total reduction is distributed across passes. If a pass takes too much at once, the strip hardens unevenly, edges can crack and local thinning concentrates damage. A balanced schedule keeps the load uniform and lets each pass close small surface irregularities rather than amplify them. The second is roll-surface condition. Rolls are ground to a controlled surface finish and kept clean; a scored, pitted or contaminated roll prints its own pattern into the foil on every revolution, and a deep mark repeated around the coil produces a recognisable banding of perforations. This is one reason roll inspection and changing intervals are treated as quality controls rather than maintenance chores.
The third variable is tension and speed. Web tension must be high enough to keep the strip flat and centred, and low enough not to neck or wrinkle it; a wrinkle that is rolled flat becomes a crease, and a crease thins the metal locally until it can perforate. Tension spikes, caused by a splice, a diameter change or a speed step, create the transverse bands of holes that quality teams learn to recognise. The fourth is cleanliness: airborne dust, mill debris, oxide flakes and lubricant residues all act as third bodies, and any one of them trapped in the roll bite will imprint the sheet. Measurement concepts used to characterise such surface features are described by the National Institute of Standards and Technology. Slitting and rewind conditions matter too, because edge damage and winding faults introduced after rolling are read as perforations on the customer's line.
From defect to through-hole
It helps to picture the defect as a race: the flaw must be present at a point where the strip is thin enough for it to cross, and it must not be healed by later passes. Most potential flaws are closed, smeared over or pushed to the surface and rolled flat. Only a minority persist, and the ones that persist are exactly what a customer's inspection finds. That is why two coils of the same alloy, gauge and width can differ in perforation level: the difference lies in rolling practice rather than in the specification on paper.
Why do pinholes matter for barrier performance in pharmaceutical and food packaging?
A pinhole is a hole through the barrier layer, so its importance is set by what the pack must keep out or hold in.
In pharmaceutical and food packaging, pinholes let moisture, oxygen and light cross the foil layer, threatening shelf life and sterility. Fewer perforations mean a more reliable barrier, so the acceptable level depends on the pack.
Dive deeper
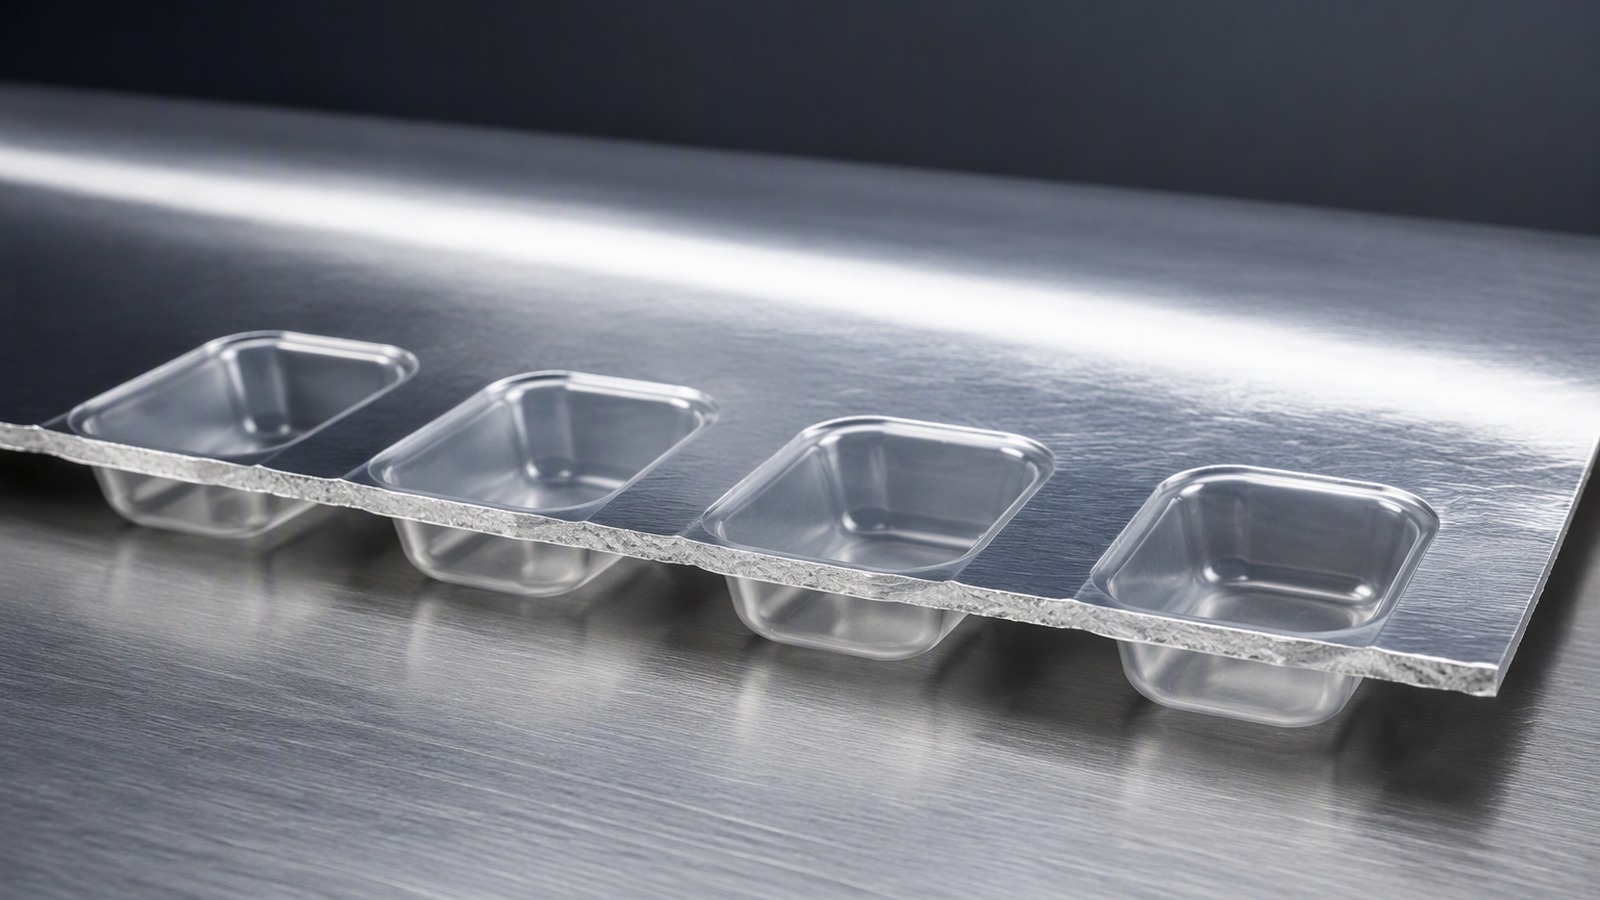
Aluminium foil earns its place in packaging because a continuous metal layer is an excellent barrier to moisture, oxygen, light and aroma, and it does so at a very low weight. That performance is a function of continuity: any through-hole is a channel. When a pinhole pierces the foil, the laminate's barrier is no longer a property of the material alone - it becomes a property of the weakest point in the sheet. For a pharmaceutical blister, the foil is the lidding that seals a cavity holding a sensitive dose; a perforation can compromise the seal's protection and let moisture enter the cavity. For a food laminate, a perforation shortens the time the pack holds its atmosphere, which can change texture, colour or flavour well before the printed date.
Barrier is not the only consequence. A perforation that opens onto the product can also be an entry point for contamination, and in sterile applications that is a direct quality concern. On the packaging line, perforations can cause leaks that fail leak testing, or let fine product dust escape. The engineering response is to reason in terms of the pack's duty: a light-blocking wrap for a non-critical item tolerates far more perforations than a high-barrier laminate for an oxygen-sensitive one. Judgements about foil's place in packaging and its recycling are maintained by European Aluminium.
Choosing the right foil for the duty
The practical route is to start from the barrier the pack needs, then work back to gauge, alloy and laminate structure. Where the duty is high, buyers choose a foil developed for pharmaceutical laminates, such as pharmaceutical aluminium foil, and where the job is a blister lidding or a sachet, a converter-grade product from our range of pharmaceutical foil for blister and sachet packaging can be specified. In both cases the same logic applies: define the barrier, then define the foil that delivers it, and treat perforation level as one measured input rather than the whole answer.
How should a buyer state a pinhole acceptance approach in a specification?
A specification should say how perforations will be judged, not merely that they exist, so that buyer and supplier measure the same thing.
State the test method, the sample and the reporting format, then agree the acceptance approach to the application rather than fixing one number. Add gauge, alloy, temper, width and packing so the basis is complete.
Dive deeper
A workable specification separates three things: the parameter, the method and the acceptance approach. The parameter is what the customer is buying - for example gauge, alloy, temper, width and core. The method is how a feature such as a perforation is observed and how it is reported. The acceptance approach is how the two parties decide, together, what result is fit for the intended pack. Writing the acceptance approach as a single number invites disputes, because a number that suits a light-blocking wrap will be either wasteful or unsafe somewhere else. Writing it as an agreed method, plus an agreed approach to the application, keeps both sides measuring and judging the same way.
In practice, a specification line might read: perforation level to be assessed by transmitted-light inspection of a stated sample size, and the acceptance approach is agreed to the application. That sentence is deliberately open on the figure and tight on the process. It tells the supplier how the sample will be taken and read, and it tells the buyer that the level will be judged against the end use rather than against a generic cap. Supporting items belong in the same document: the alloy from those available, the temper, the thickness in millimetres, the width in millimetres, the core diameter, the packing method - eye to sky or eye to wall on wooden pallet with moisture barrier wrap - and the ports from which the material is shipped.
Making the specification enforceable
For the approach to work, both parties must agree the sample plan, the lighting condition and the reporting units before the order, because a result is only meaningful against a stated method. Standardised terminology for light metals helps keep the language consistent; the frameworks maintained by the ASTM Committee B07 on Light Metals and Alloys are a useful reference point for how such properties are described. Where the pack is a pharmaceutical blister, the same discipline is applied end to end, as described in our guide on how to specify pharmaceutical blister foil: define the duty, define the method, and let the acceptance approach follow the application.
How should pinholes be checked on received material?
Checking on receipt is about a repeatable, safe method that any inspector can follow, not about a single pass-or-fail figure.
Inspect received foil by transmitted light on a defined sample, count and record what is seen against the agreed method, and compare the result with the acceptance approach agreed for the pack. Record the sample, the light source and the viewing conditions.
Dive deeper
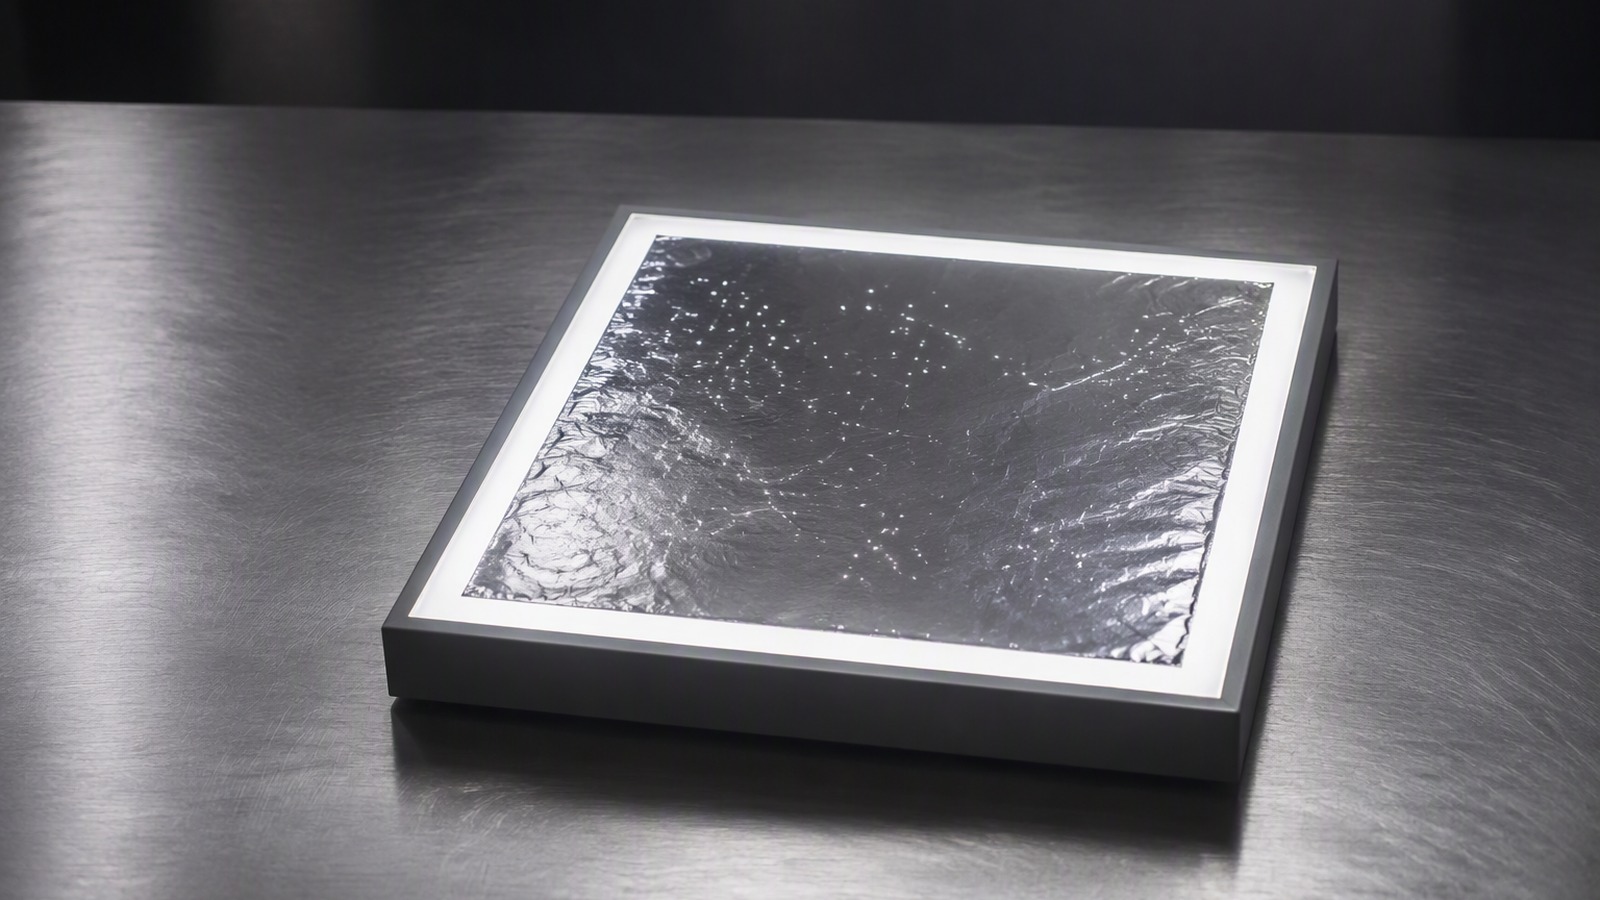
Receiving inspection should be simple enough to be repeatable and strict enough to be meaningful. The common method is transmitted-light inspection: the foil is placed so that light passes through it, and any perforation appears as a bright speck against the darker background of intact metal. The method catches through-holes reliably and is quick, but it must be controlled to be comparable over time. That means fixing the sample size and location, the light source and intensity, the viewing distance and the ambient light, because a perforation seen under one set of conditions may be invisible under another. Ideally the same method is used by supplier and customer, so results can be compared directly.
Two cautions apply. First, inspect the sample in a way that protects it: finger marks, creases and dust introduced during handling can create apparent defects or hide real ones, and unpowdered gloves plus clean handling keep the result honest. Second, treat the result as data, not as a verdict. Record the sample identity, the coil, the method and the observed level, and compare against the agreed approach rather than against an isolated figure. Over several deliveries, the pattern tells a buyer whether the specification is being met consistently or whether coil-to-coil variation needs attention.
Building a repeatable routine
A practical routine has four steps. Agree the sample plan with the supplier before the first delivery, so both sides look at the same slice. Fix the inspection set-up so the light source and viewing conditions never drift. Record results on a simple form that carries the coil number, the method and the observed level. Finally, review trends at the quality meeting, and where results drift, revisit whether gauge control, handling or the specification itself needs adjustment. Treated this way, pinhole checking becomes part of normal incoming inspection rather than a special test, and it feeds directly back into the specification the buyer wrote.
Pinholes come from gauge, alloy and rolling practice; because their importance depends on the pack, acceptance is agreed to the application and checked on every delivery.